Taiwan-made · Established 2008 · ISO 9001:2015 (TÜV SÜD)
Taiwan Cold Forging Machinery & Custom Tooling Partner for Fastener Manufacturers
From bolt formers, nut formers, thread rolling machines to custom punch pins and tooling, GoldPlus helps fastener manufacturers source reliable Taiwan-made machinery and tooling for standard and non-standard production.
What we help you source
One partner for cold forging machinery and fastener tooling
GoldPlus supplies the machines and the tooling that fastener manufacturers need — and helps you choose the right setup for your parts.
Cold Forging Machinery
Bolt formers, nut formers, and heading machines for standard and non-standard fastener forming.
Explore solutionFastener Tooling
Trimming dies, wire drawing dies, thread rolling dies, and custom tooling built from your drawing.
Explore solutionProduction Accessories
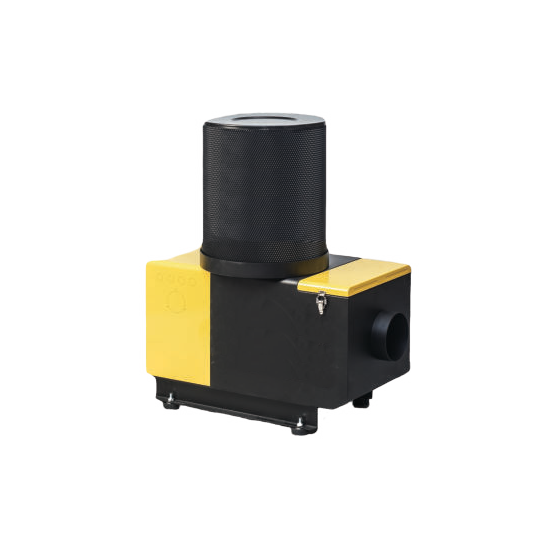
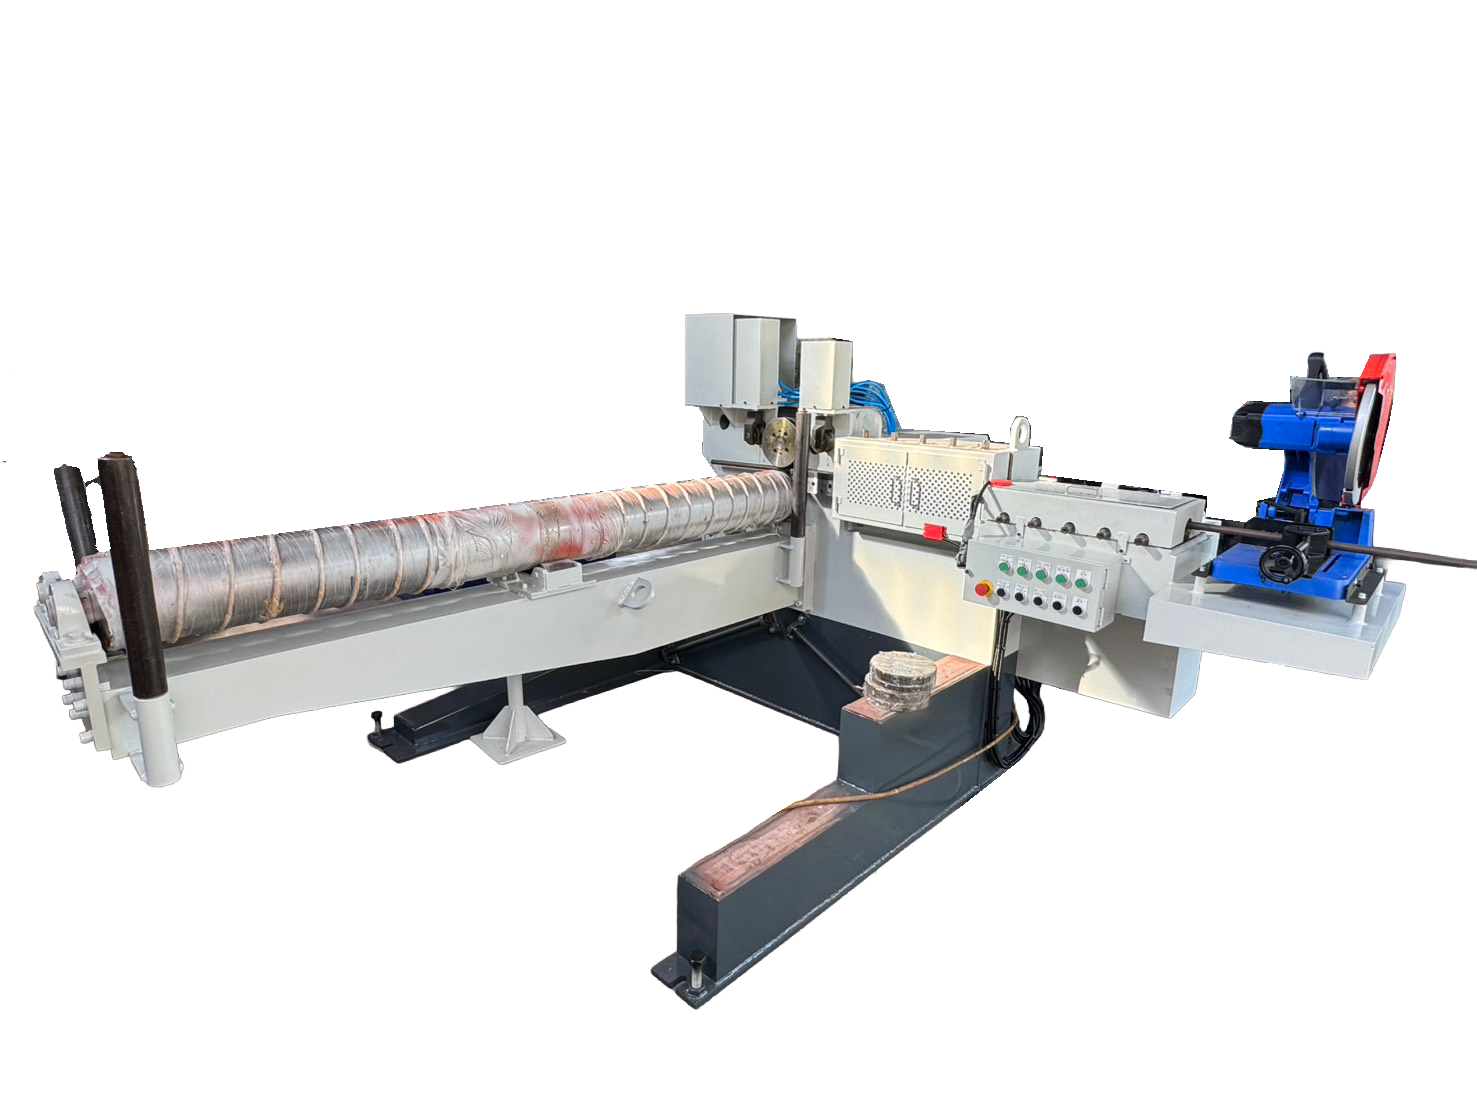
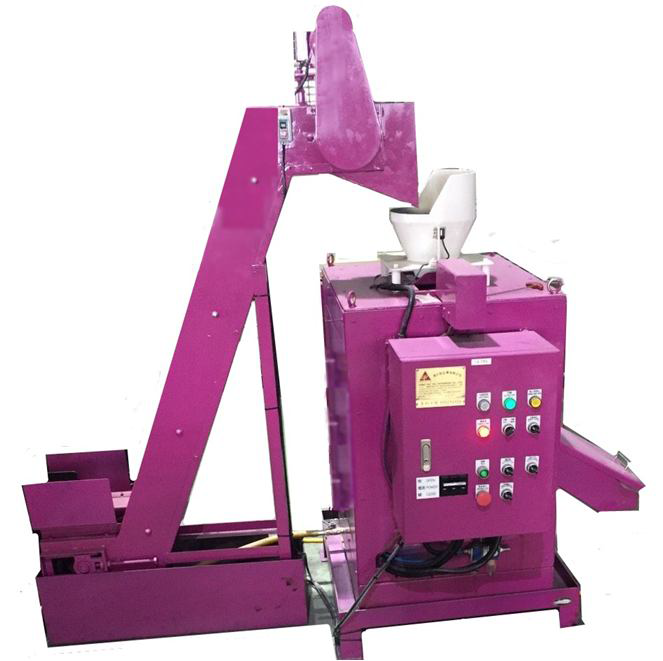
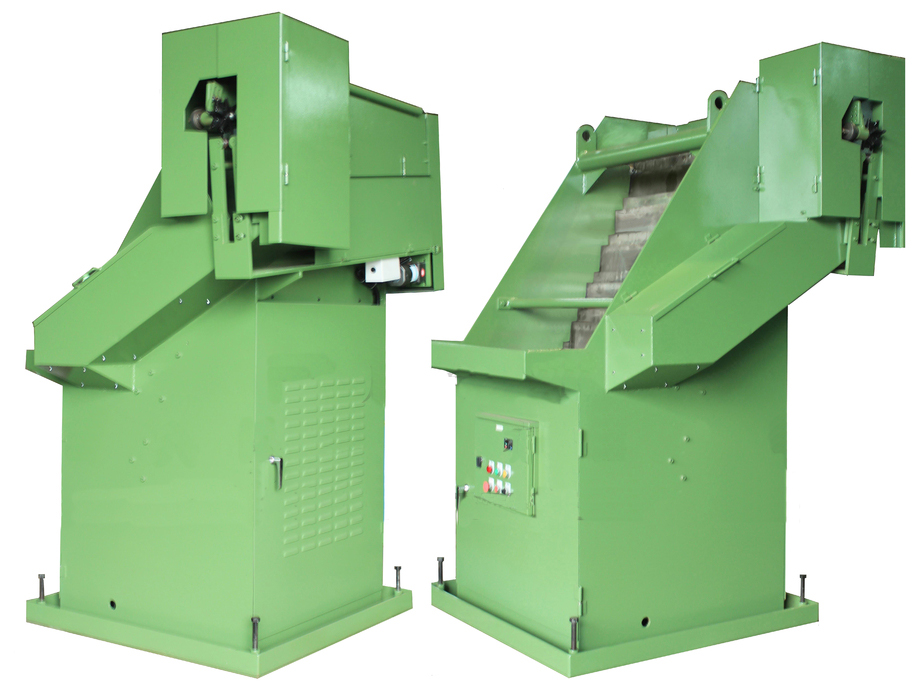
Screw straighteners, oil mist separators, and centrifuge cleaners that keep a fastener line running clean and steady.
Explore solutionBuilt for fastener manufacturers
Who we work with
GoldPlus works with fastener producers and sourcing teams who need dependable Taiwan-made machinery and tooling.
- Bolt manufacturers
- Nut manufacturers
- Automotive fastener suppliers
- Electronics fastener suppliers
- Custom fastener manufacturers
- Trading companies sourcing Taiwan machinery
Machinery
Cold forging machinery
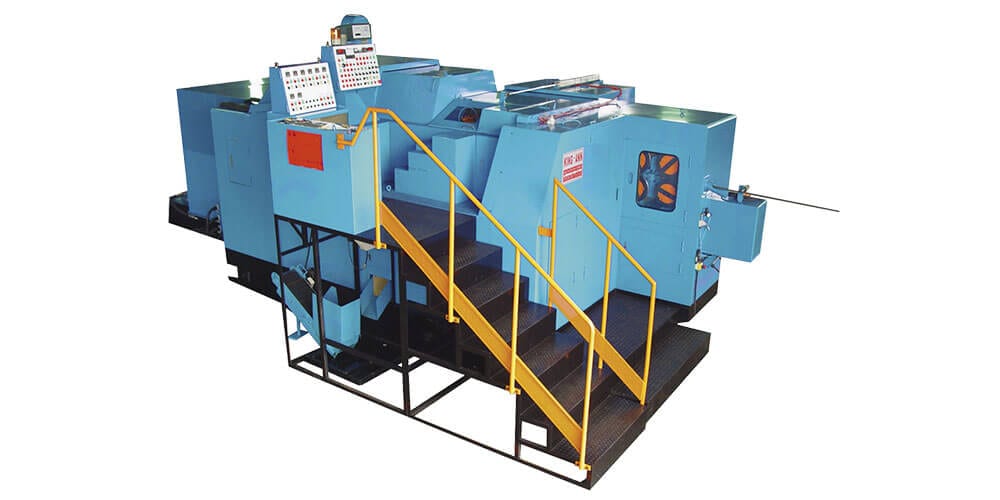
Bolt Former
Taiwan-made bolt formers in 3, 4, and 5 station configurations, with extra-long kick-out options for special applications.
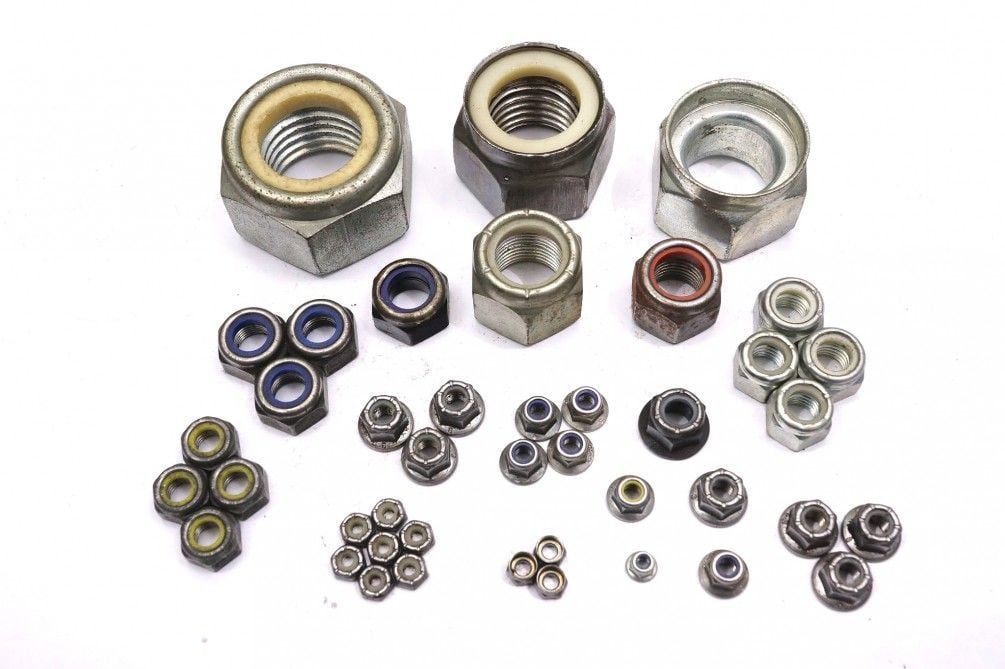
Nut Former
Automatic nut formers in 5, 6, and 7 station configurations, including punch kick-out models for special nuts and custom cold forged parts.
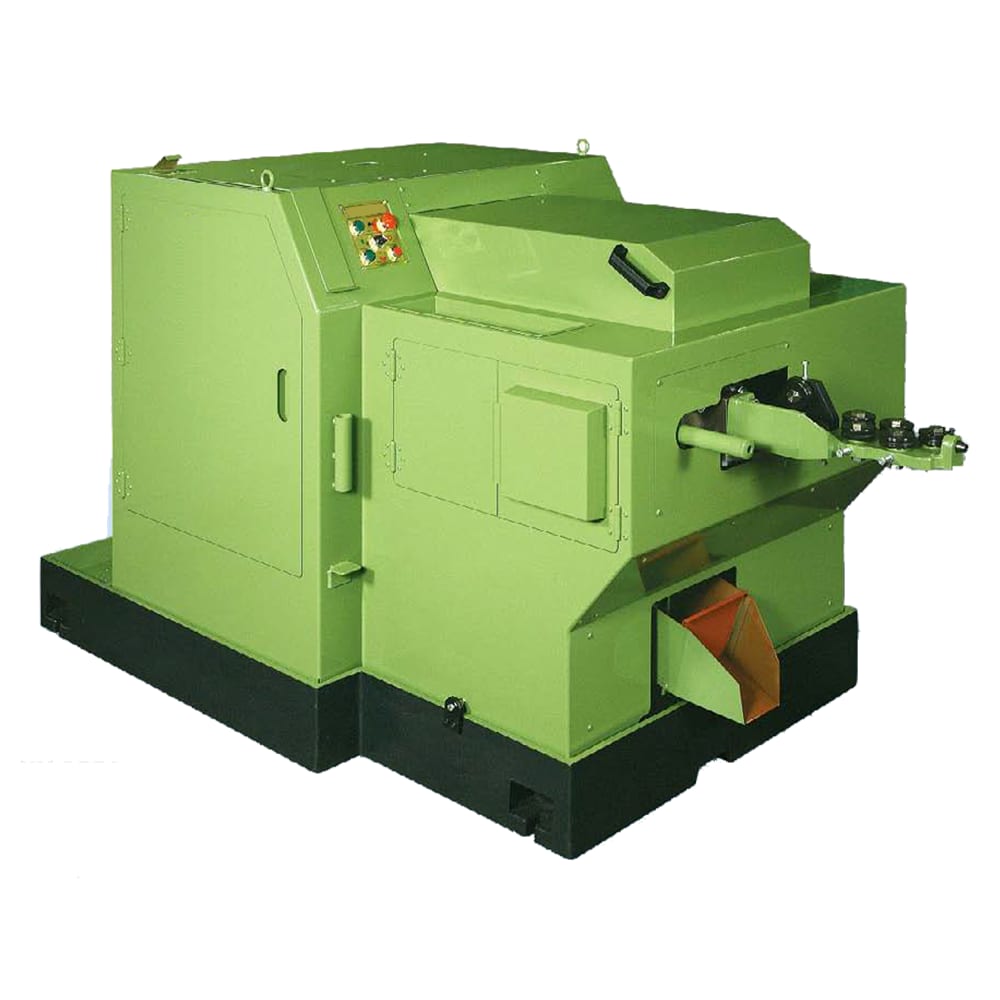
Heading Machine
Reliable cold heading machines, including 1 die 2 blow configurations, for standard and non-standard part production.
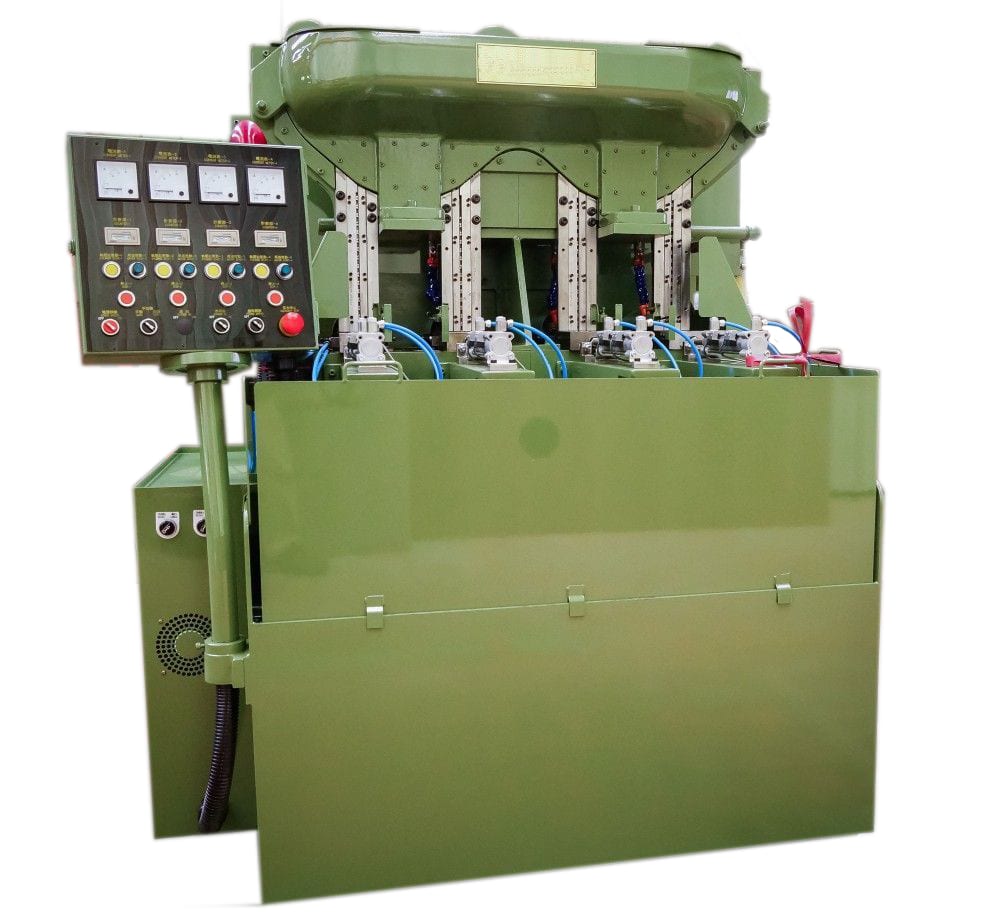
Tapping Machine
Automatic tapping machines for internal threading of nuts and threaded components.
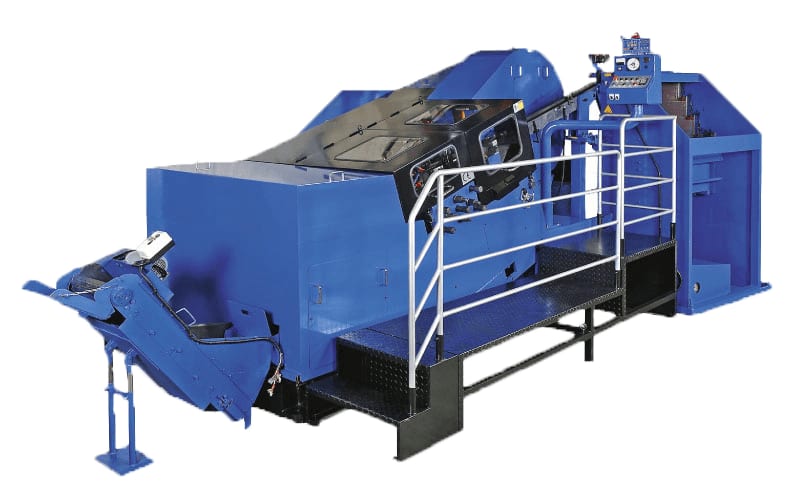
Automatic Threading Rolling Machine
Designed to improve thread quality, production stability, and operating efficiency — and to work in line with bolt formers for high-volume fastener production.
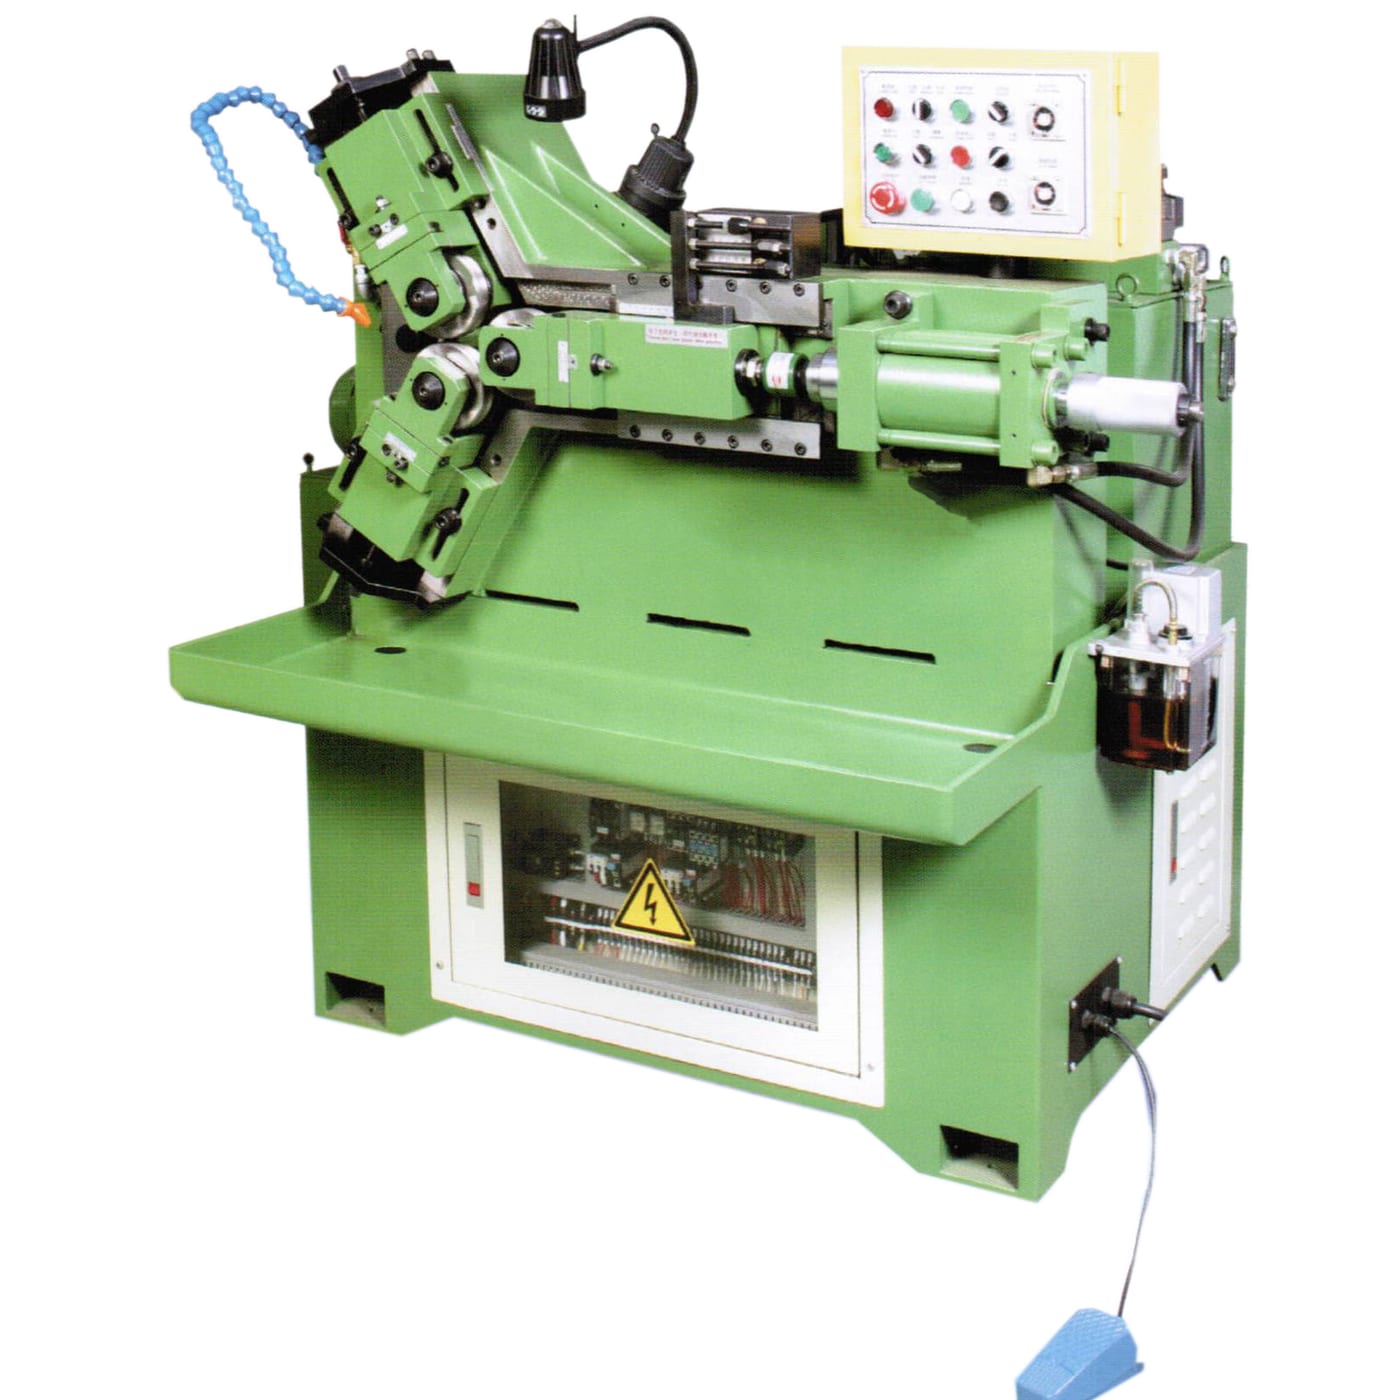
Circular Thread Rolling Machine
Through-feed, in feed, 3-die pipe type, and cam in-feed configurations for screws, bolts, tubular, bicycle, and automobile parts.
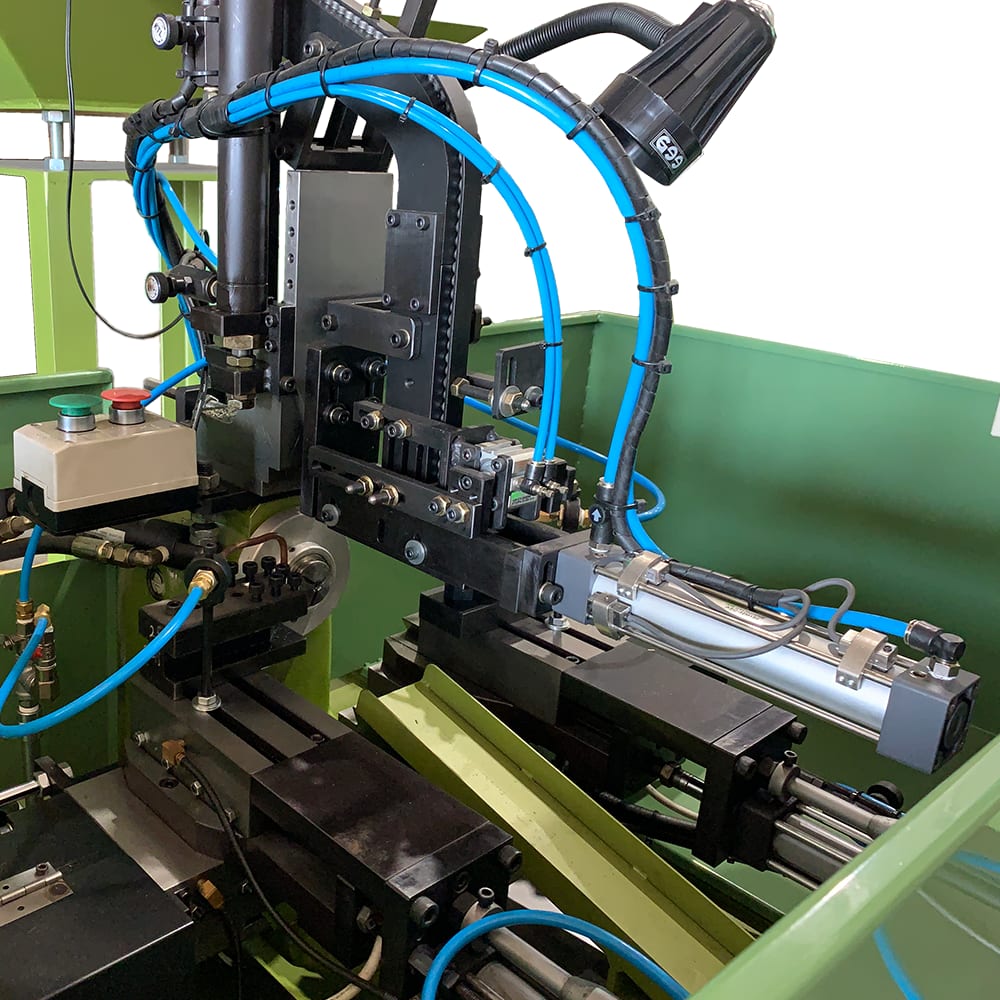
Secondary Processing Machine
Point cutting, end chamfering, drilling, and related secondary operations to complete your fastener production line.
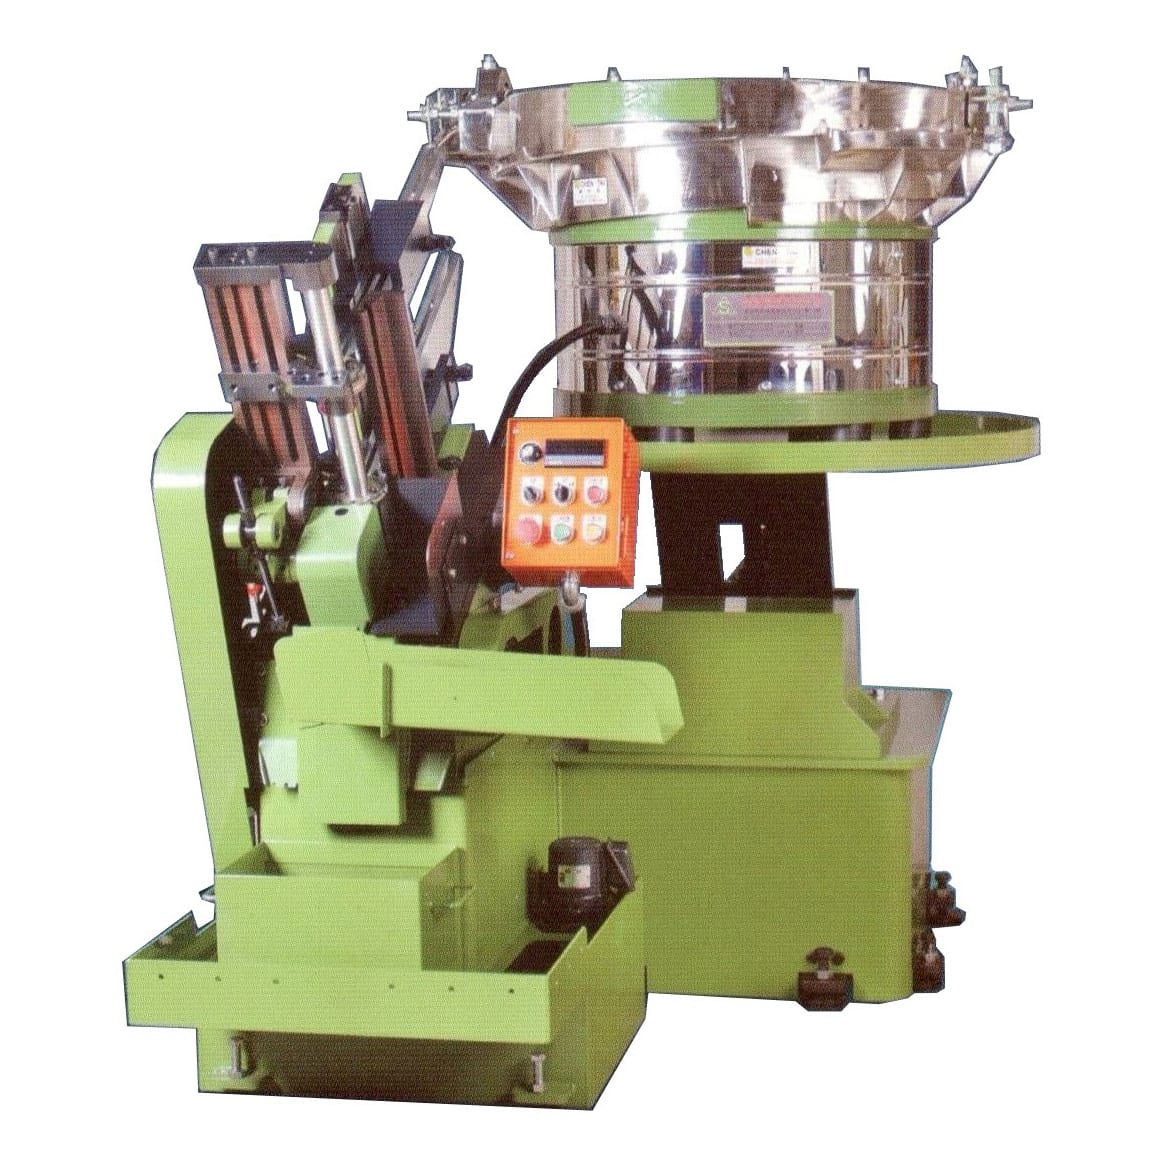
Point Cutting Machine
Point cutting operations as part of the secondary processing line.
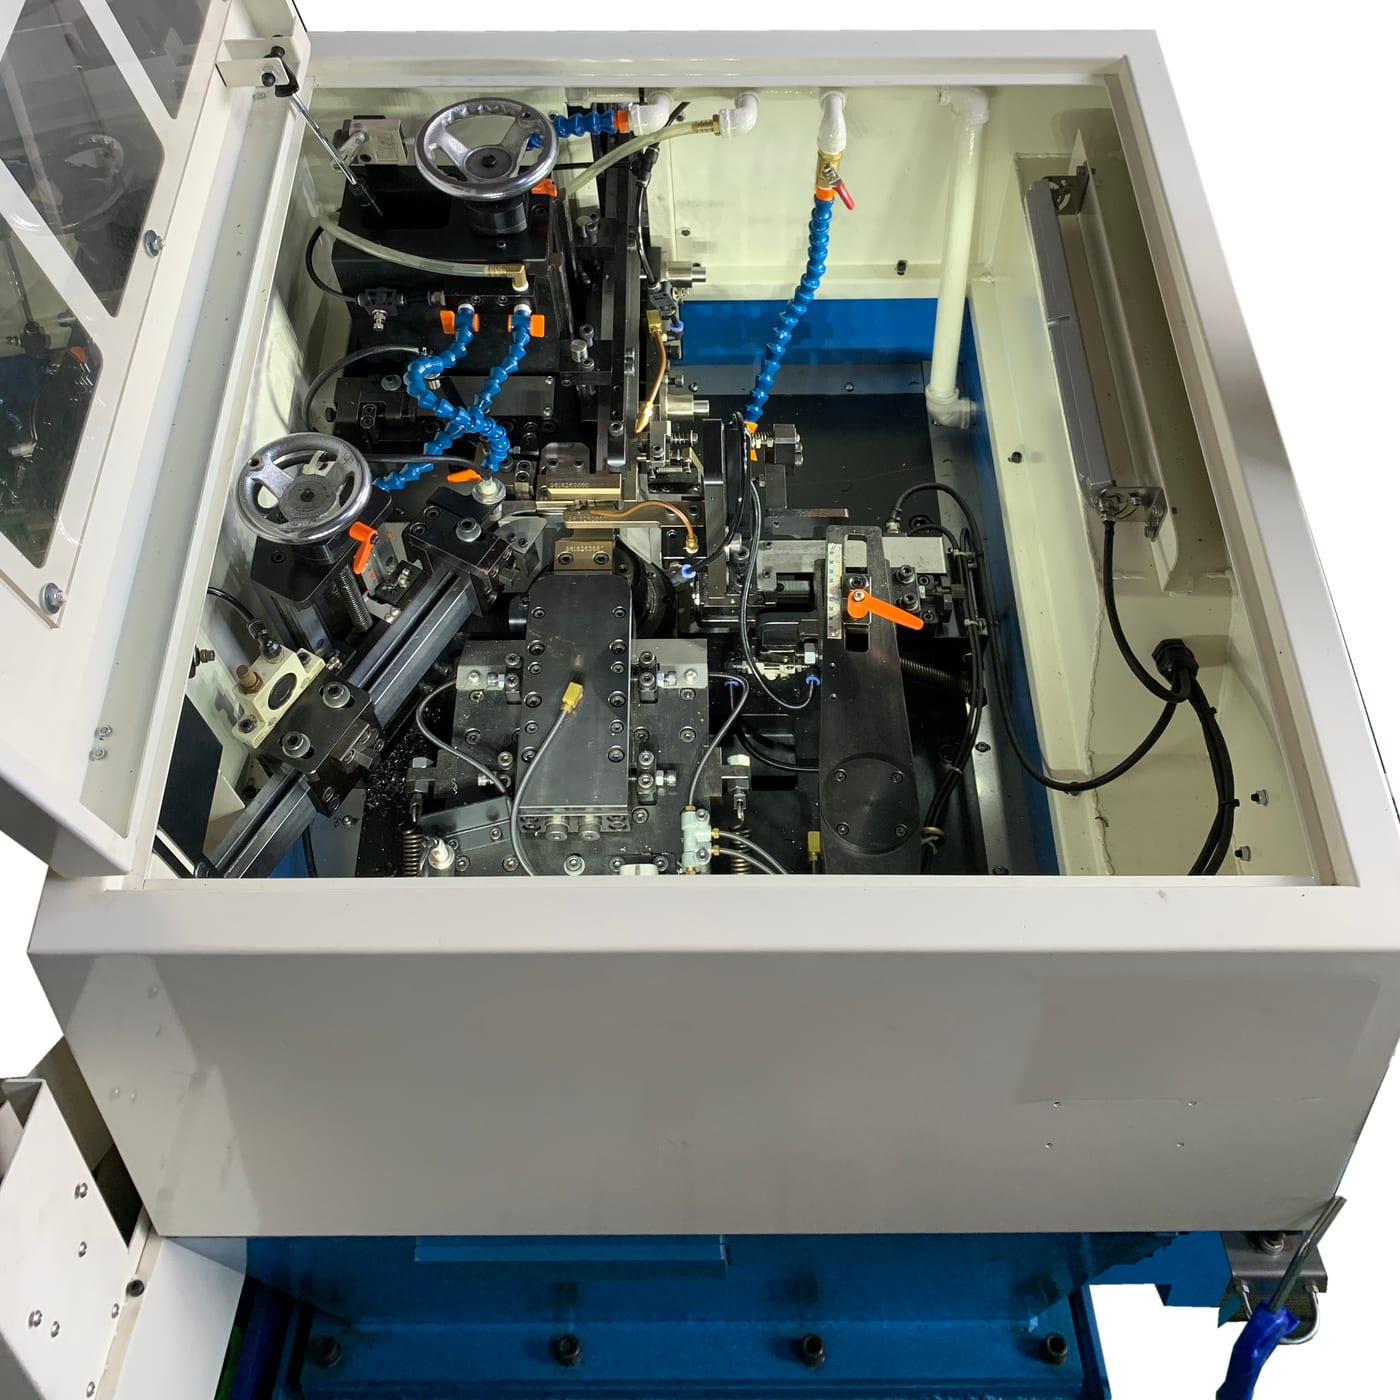
End Chamfering & Drilling Machine
End chamfering and drilling operations to finish threaded and formed parts.
Tooling
Fastener tooling
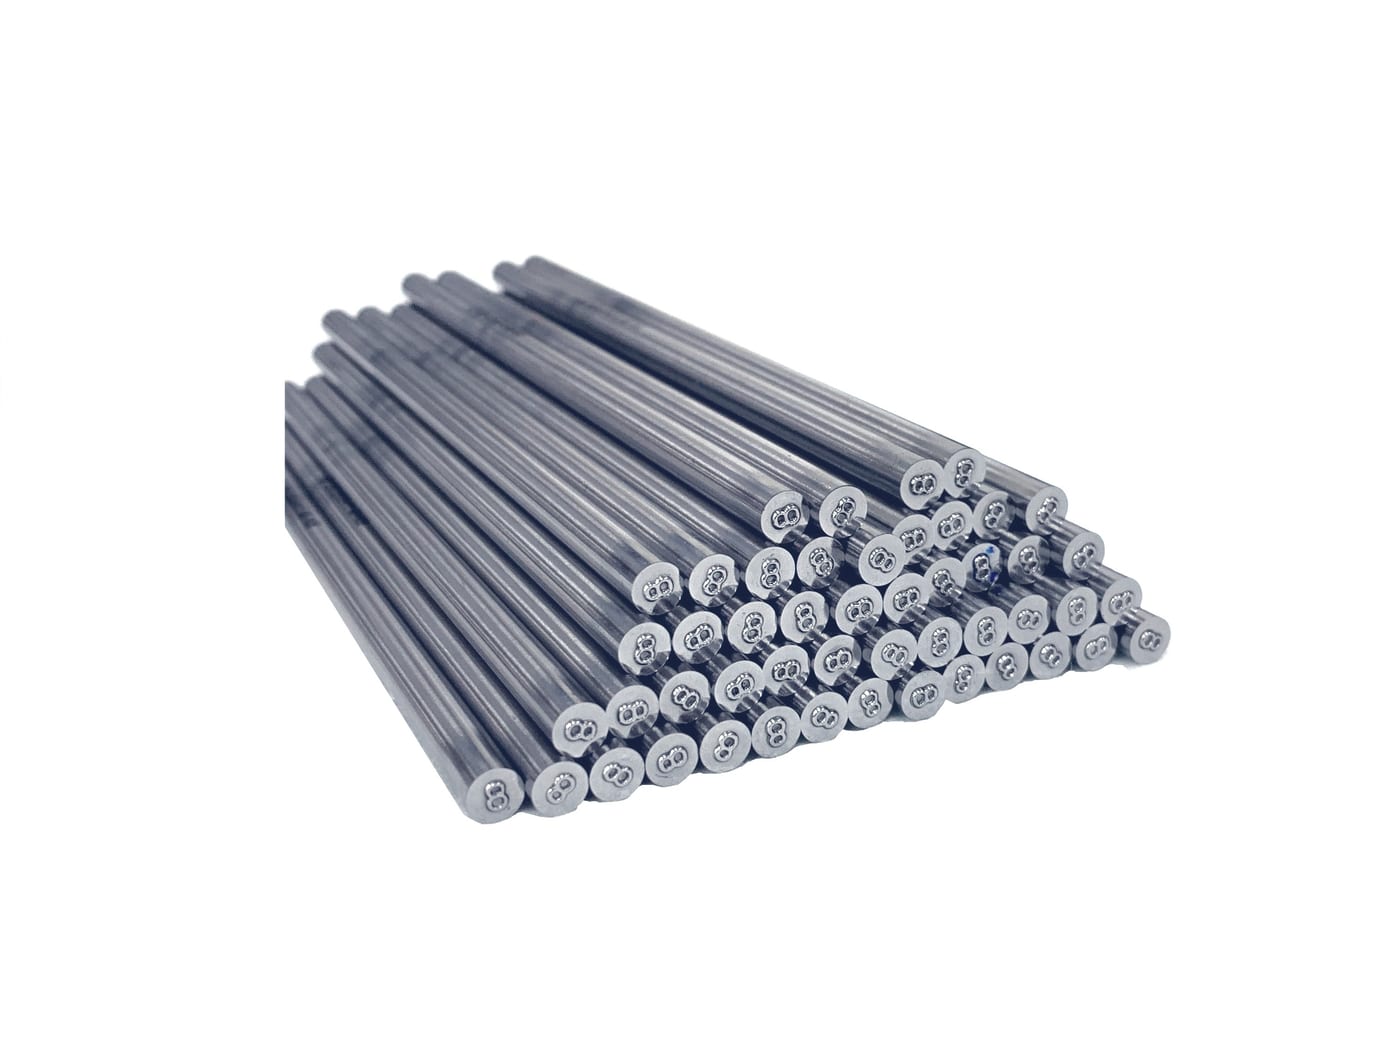
Punch Pins
Hexagon, 6-lobe recess, custom shape, knockout, nut forming, and extrusion punches with material and coating options to suit your production.
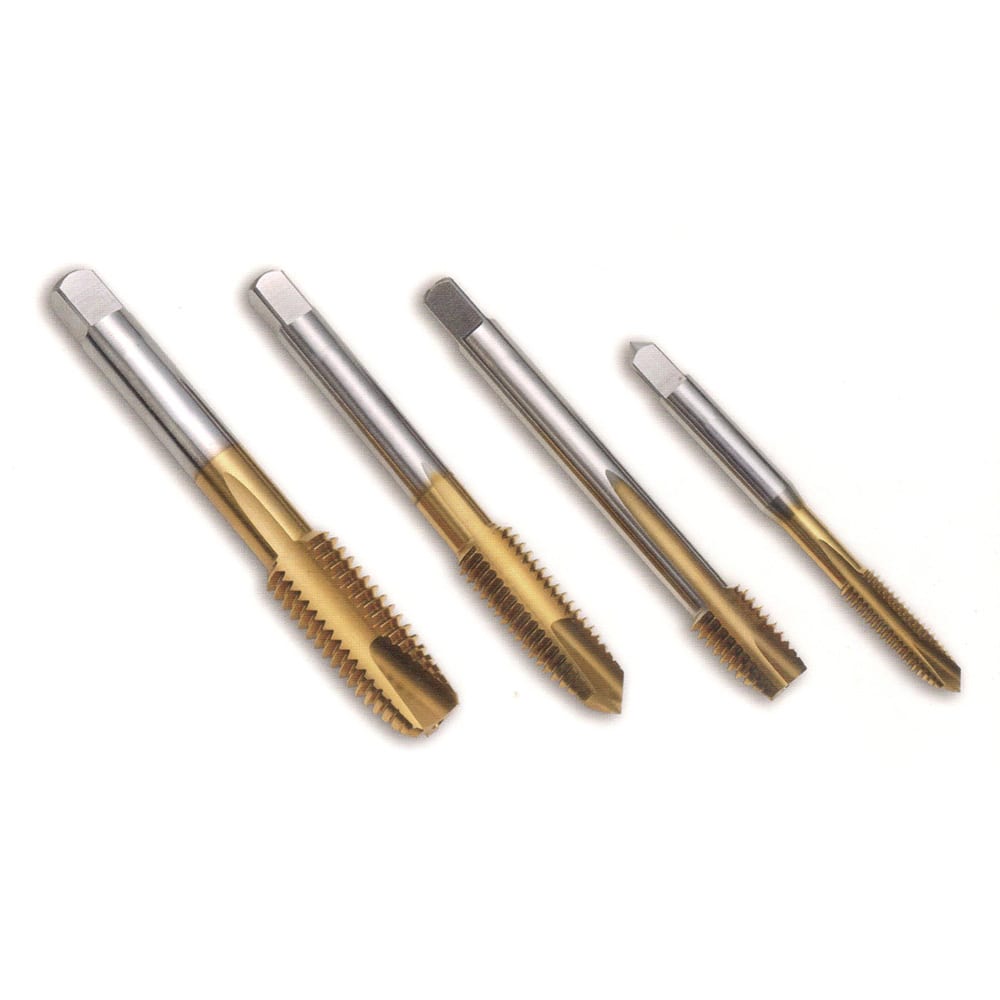
Taps
Taps for nut tapping and internal threading operations, selected by thread specification and material.
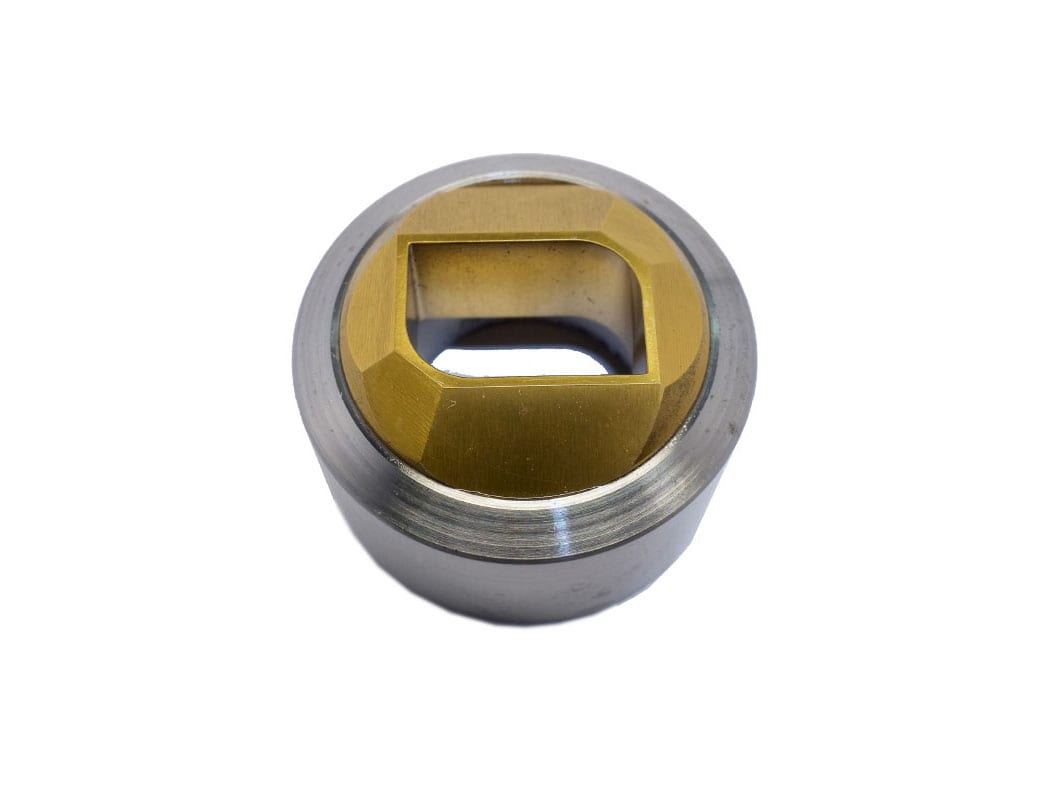
Trimming Die
Trimming dies for hexagon and shaped bolt heads, matched to your former and part geometry.
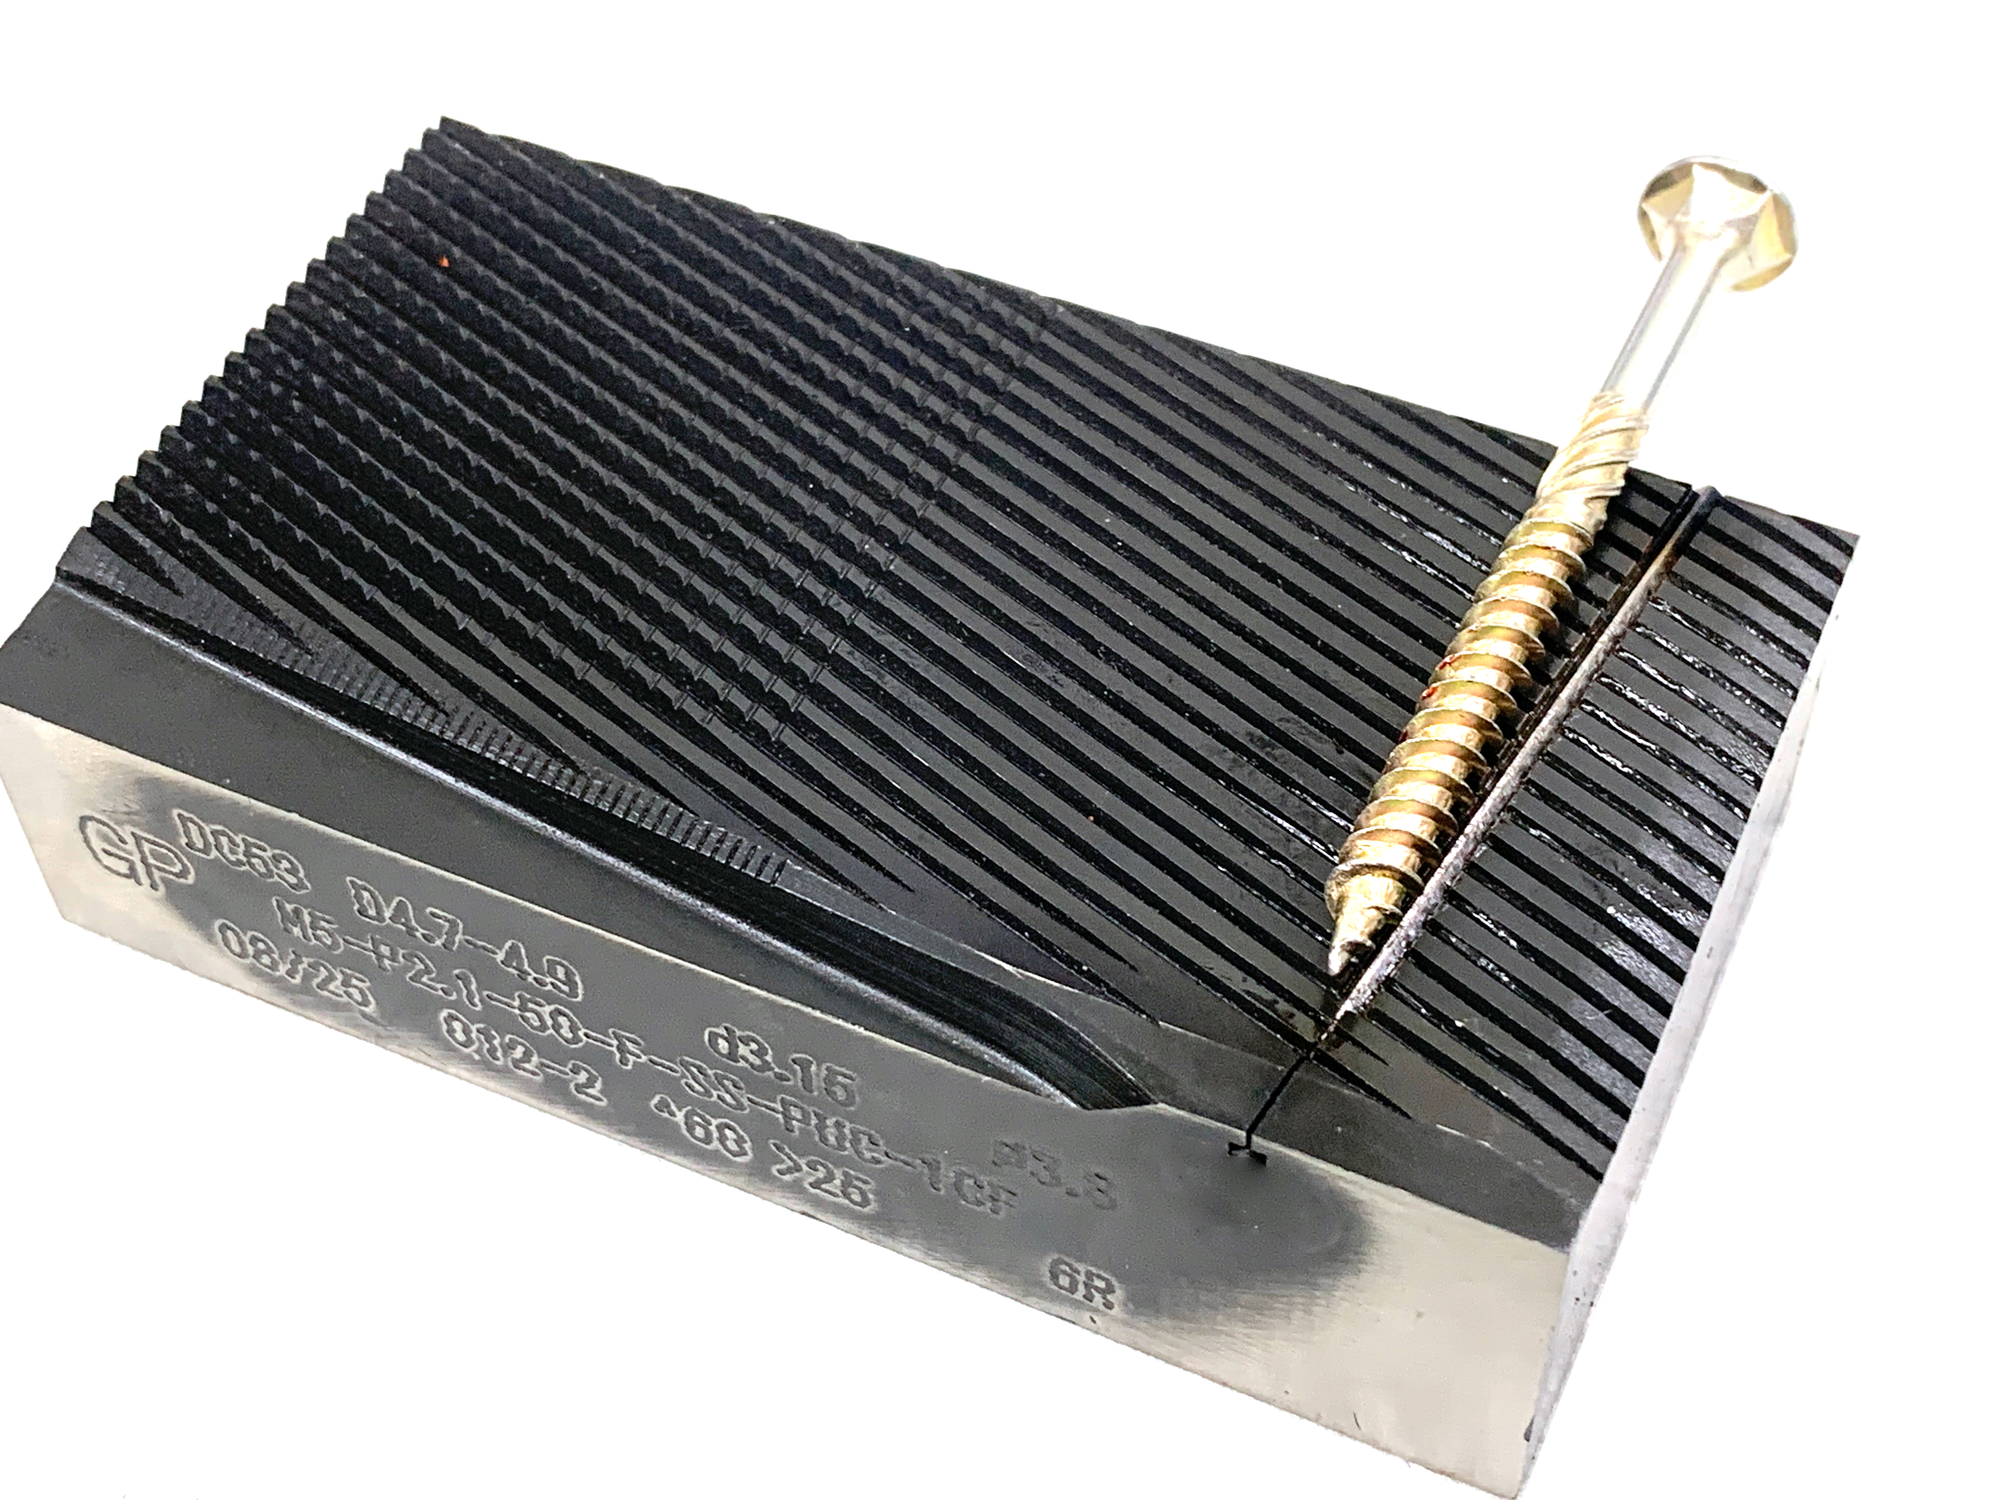
Thread Rolling Dies
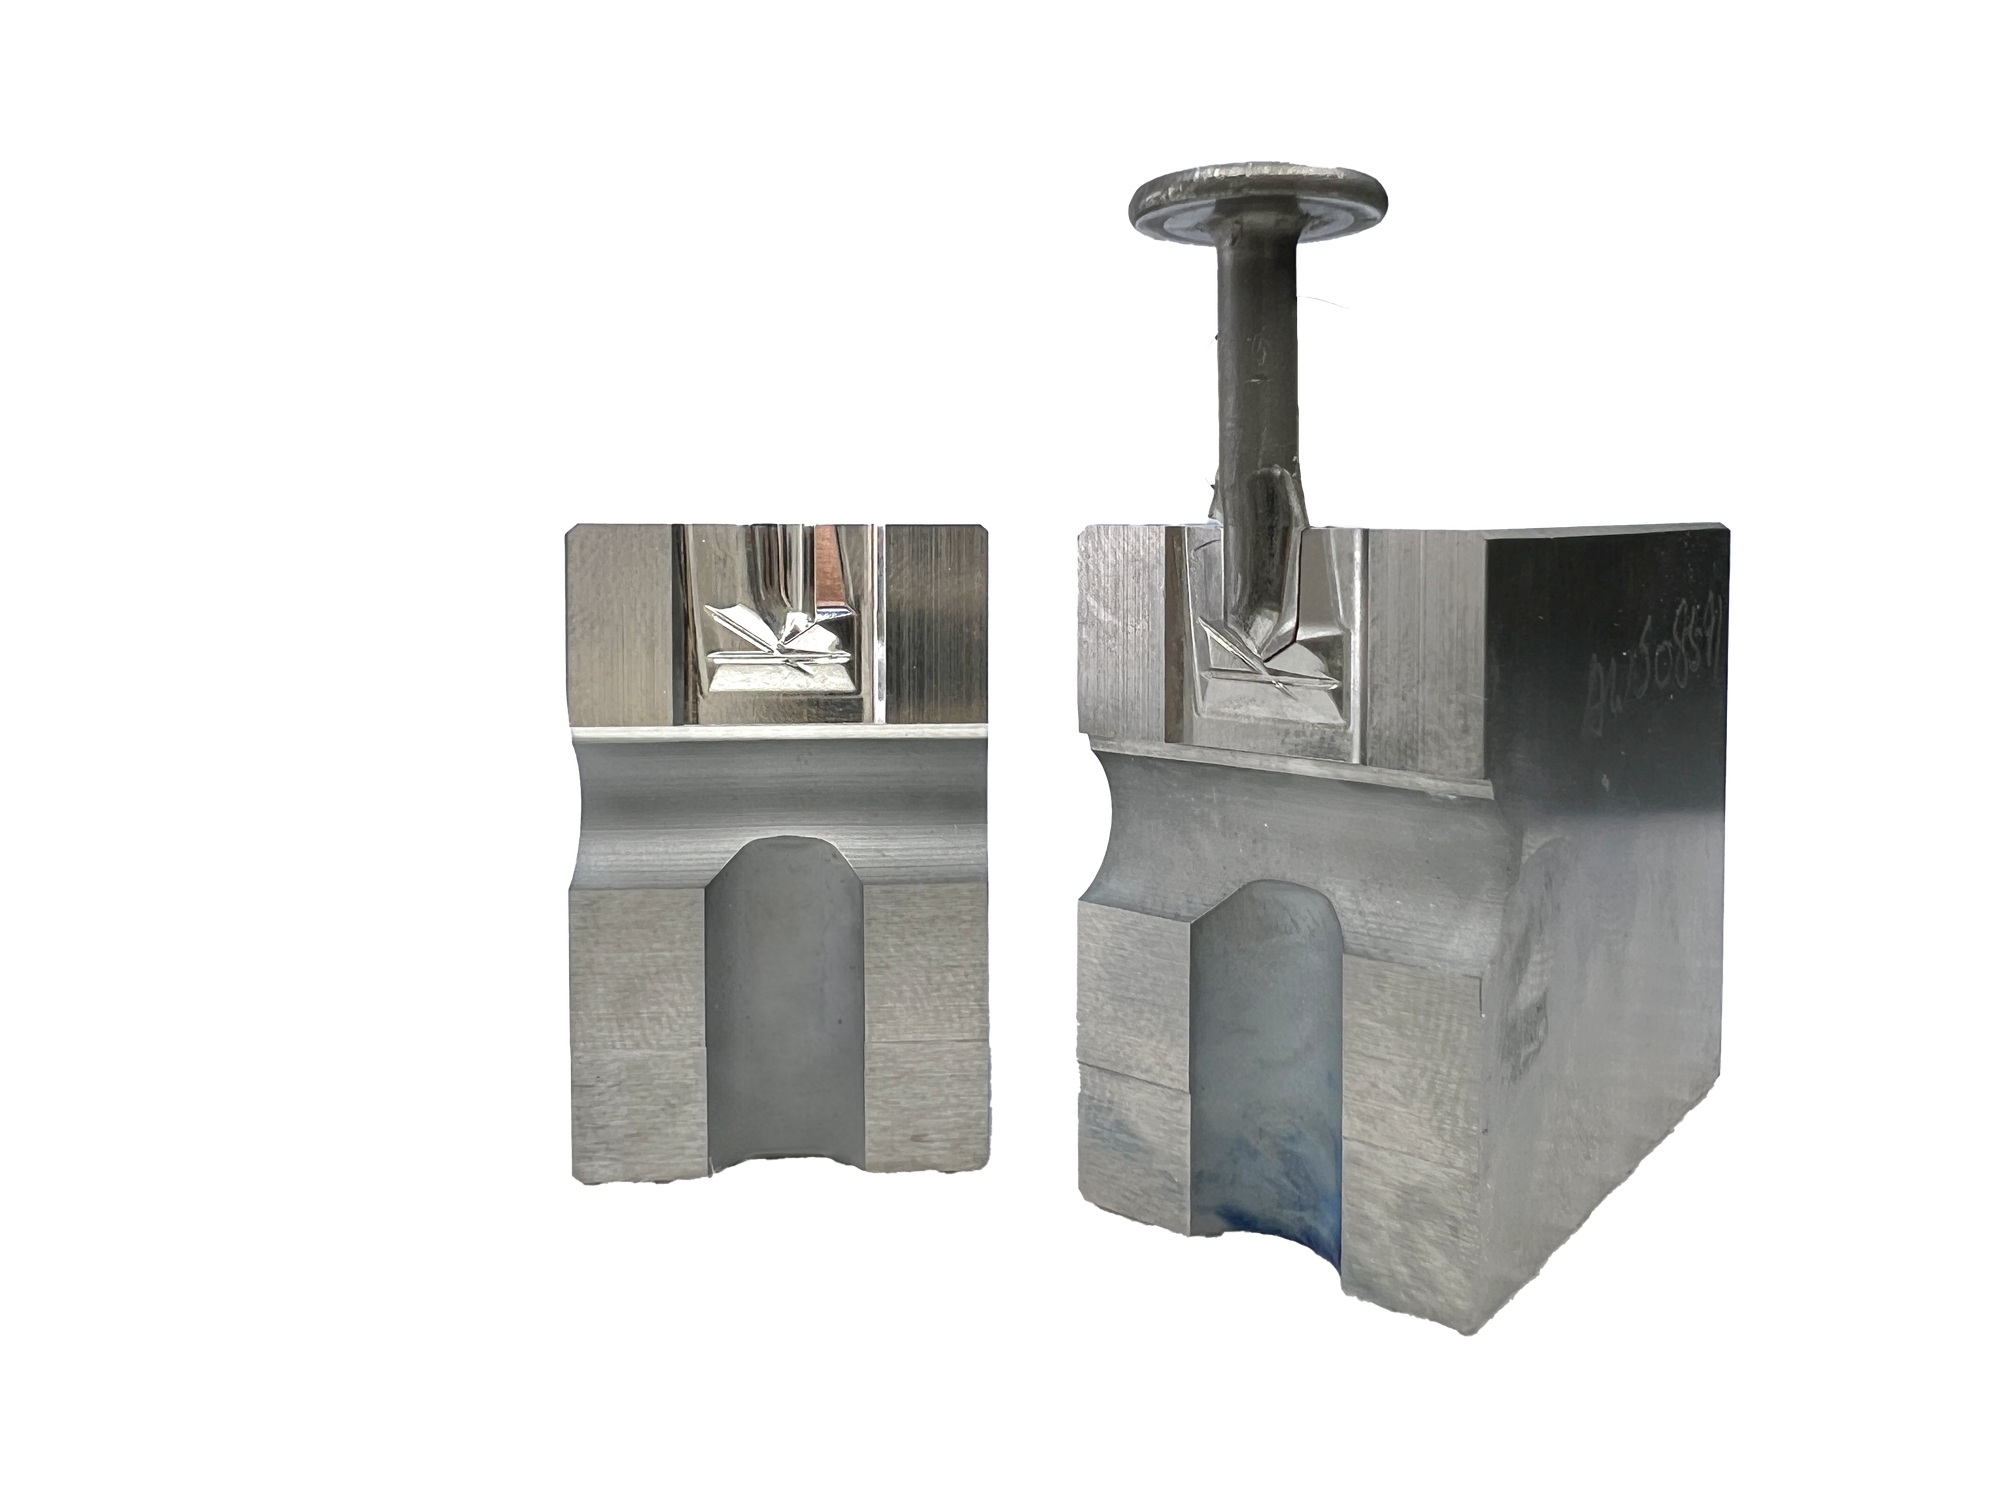
Self Drilling Screw Clamping Dies
QSD System
Coming Soon
Coming Soon
Coming Soon
Accessories
Production Accessories
Quality control
Dimensions checked before shipment
GoldPlus supports quality control with inspection equipment and can provide a printed QC report upon request.
TÜV SÜD
- Formtracer / contour measurement
- Rockwell hardness testing
- 2.5D projector
- Calipers, micrometers, holtests, pin gages
- QC report available upon request
Previous Projects
From drawing to finished part
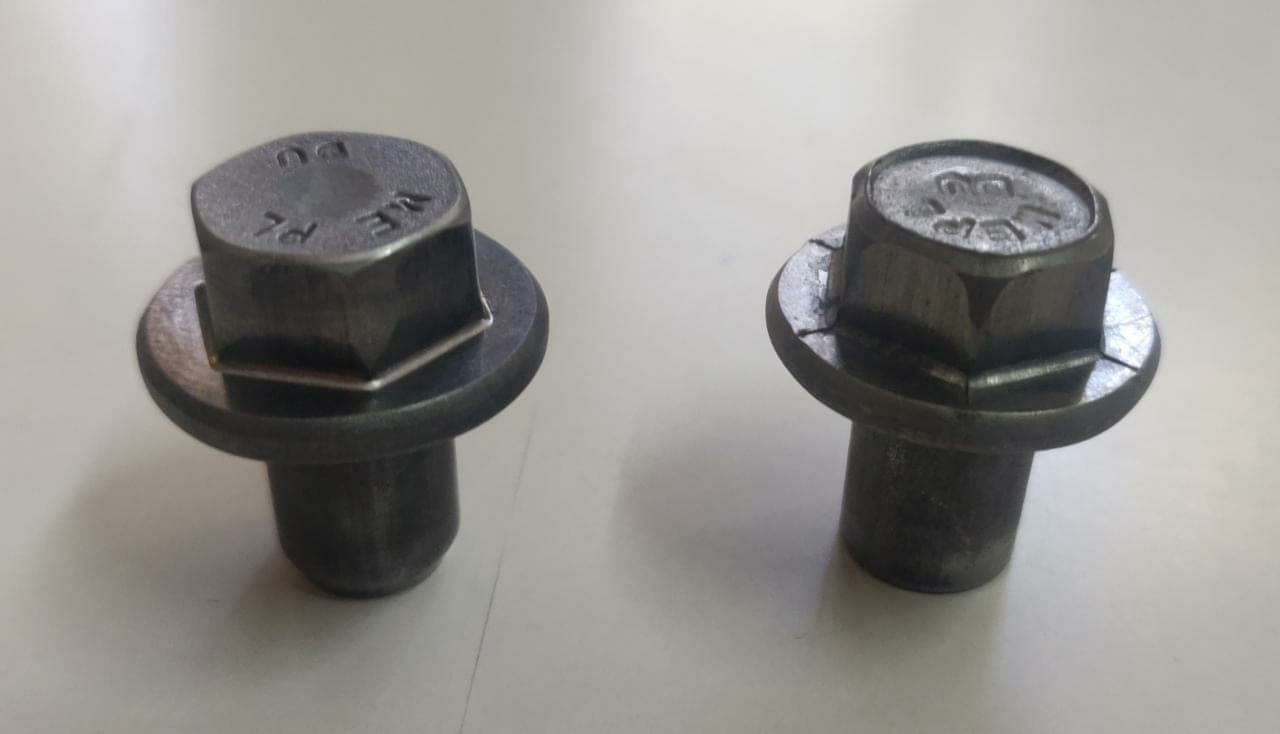
Cleaner Hex Flange Heads with the Extrusion Punch
The parts on the left were formed with our extrusion punch; the parts on the right with a conventional punch. With our punch, material flows evenly into the hex and flange. Hex corners fill completely, the flange edge stays smooth and round, and the cracks and folds at the hex-to-flange transition are eliminated. The result is a stronger, better-looking head, fewer rejects, and less secondary trimming or inspection.
Read case study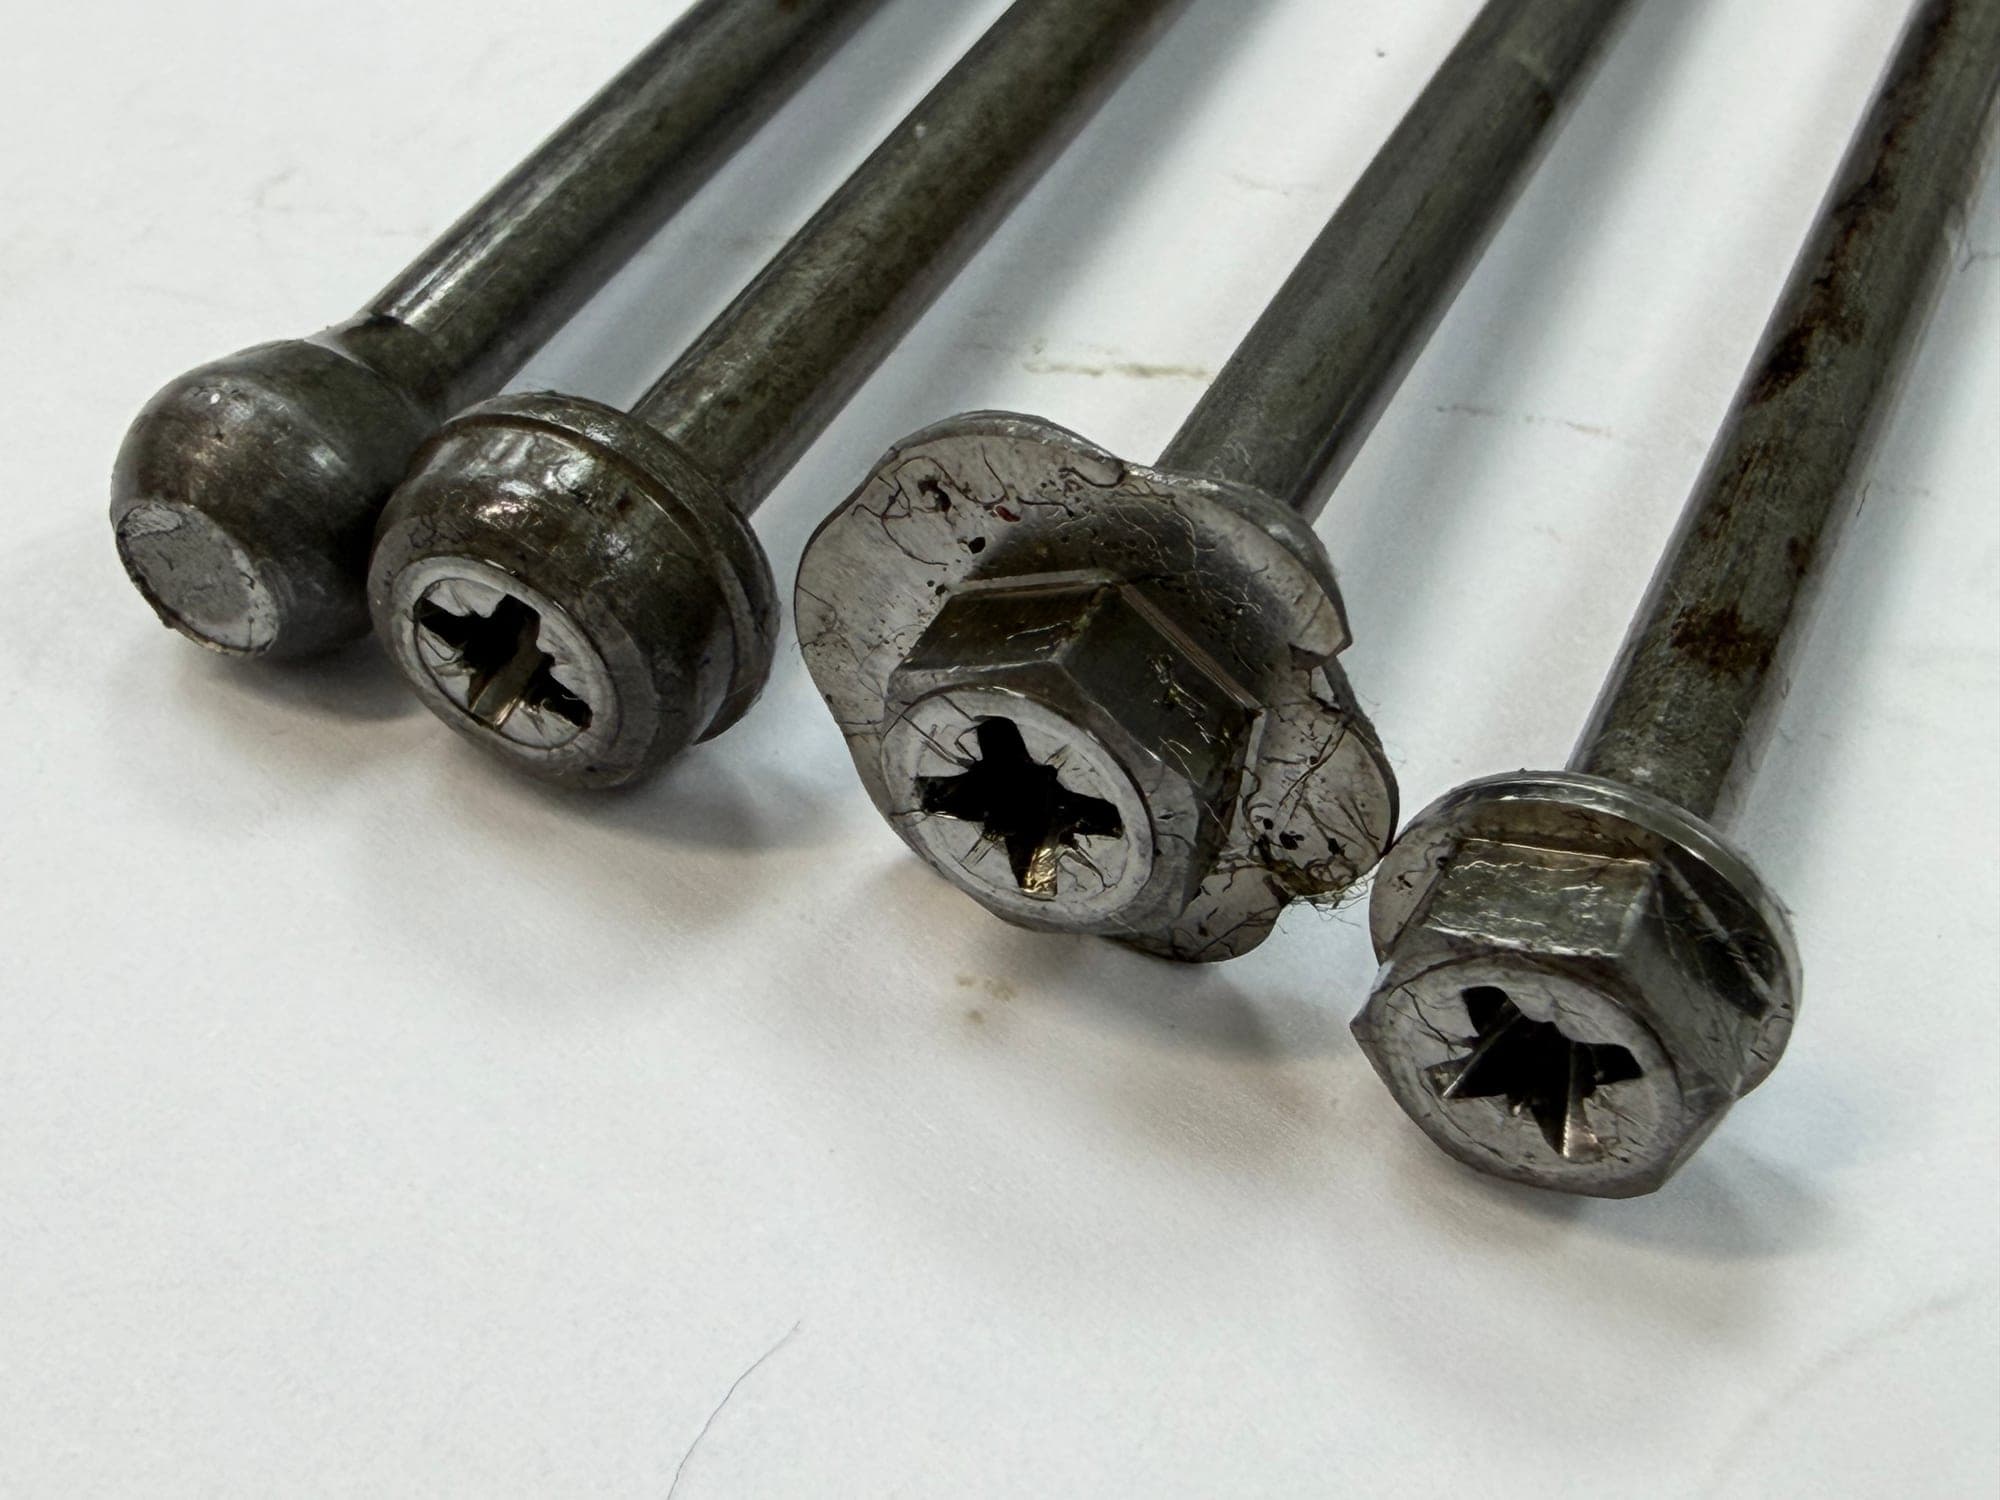
Double Trim - Hex Flange Head Screw with Pozi Recess
cold heading stage: rounded preform, round head with cross recess, trimmed hex head with untrimmed flange, and finished trimmed flange head.
Read case study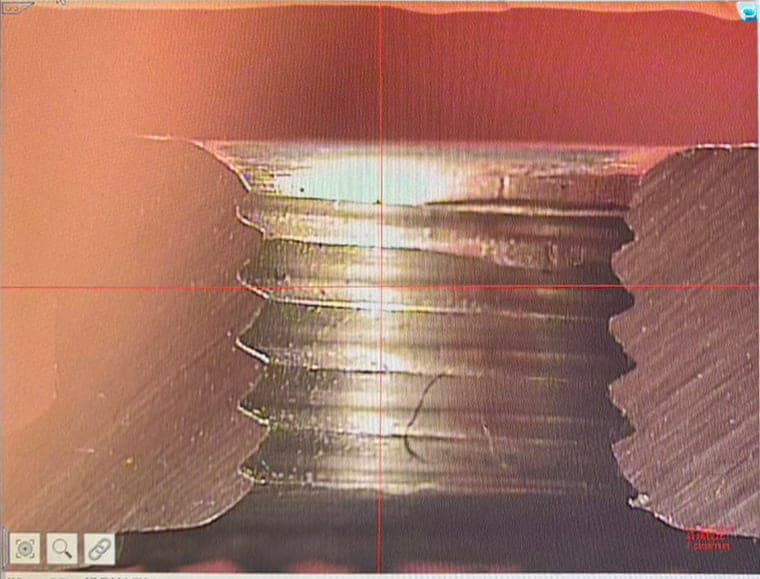
Feed Mismatch in Tapping
In tapping, the tap has to advance exactly one thread pitch for every revolution. Feed mismatch happens when the machine’s feed rate doesn’t match the tap’s pitch, so the tap advances too fast or too slow. When that happens, the machine pushes or holds back the tap as it cuts. The tap loads one flank more than the other, which leads to: Oversize or distorted threads that fail go/no-go gauges Torn or rough flanks that weaken the thread Inconsistent profiles from one hole to the next Excess tap wear and breakage from added axial stress
Read case studyHave a part drawing or machine requirement?
Send us your drawing, target production speed, material, and product dimensions. Our team will help review the suitable machine and tooling setup.
Company brochure
Our machinery and tooling range, in one document
Machines, tooling, capabilities, and quality control — the overview to share with your engineering and purchasing team.
PDF · 0.4 MB